What Is Front-End-of-Line (FEOL) Processing?
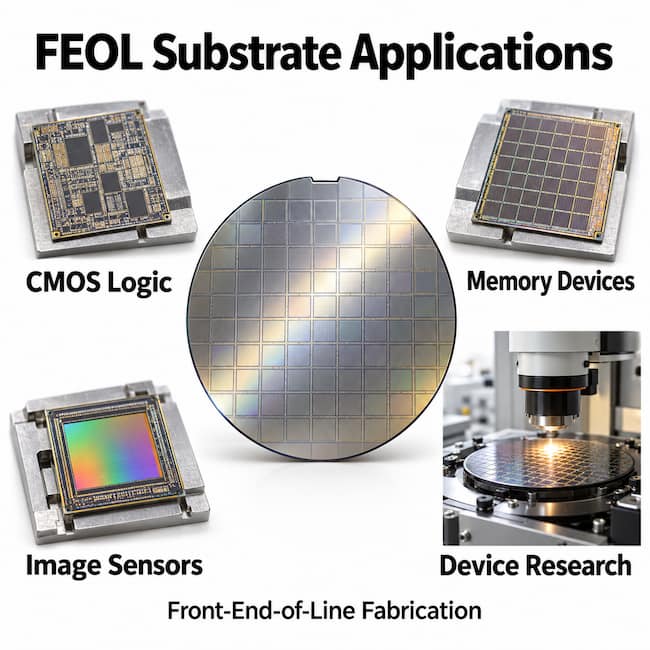
Front-end-of-line processing, commonly called FEOL, is the part of semiconductor fabrication that creates transistors and other active device structures in and on a wafer. These structures provide the switching and signal-control functions used in integrated circuits. In silicon-based manufacturing, FEOL establishes features such as electrically isolated device regions, transistor channels, gate structures, and source and drain regions.
FEOL is central to CMOS semiconductor fabrication, where complementary n-channel and p-channel transistors work together. The process depends on precise control of materials, dimensions, surface cleanliness, and electrical properties.
Request Wafers for FEOL Process Development
Use the form below to describe your substrate requirements. Include wafer diameter, thickness, orientation, conductivity type, resistivity, surface finish, oxide requirements, and quantity. You can also browse available wafers online for semiconductor research and process development.
Get Your FEOL Research Wafer Quote FAST!
Or,
Buy Semiconductor Wafers Online
and Start Researching Today!
Key Processes in FEOL Semiconductor Fabrication
A FEOL process flow combines repeated patterning, material growth, deposition, removal, and thermal treatment steps. The sequence varies with the transistor architecture and manufacturing technology. Common operations include:
- Wafer preparation and cleaning: Preparing the starting surface and removing particles, organic residues, and unwanted contamination before critical processing steps.
- Oxidation and isolation: Using insulating materials to separate device regions. Thermal oxidation of silicon grows silicon dioxide directly from the silicon surface.
- Photolithography and etching: Photolithography defines patterns in photoresist. Subsequent etching transfers selected patterns into the underlying material.
- Thin-film deposition: Adding dielectric, semiconductor, or conductive layers. Thin-film deposition methods include chemical vapor deposition and atomic layer deposition, depending on the material and structure.
- Doping and annealing: Ion implantation introduces dopants into selected regions. Subsequent annealing helps activate dopants and repair implantation damage.
How FEOL Forms a Transistor
In a MOSFET, the gate controls current through a semiconductor channel between the source and drain. FEOL processing creates the physical structures that make this control possible, including the gate dielectric, gate electrode, and doped source and drain regions. These features are fundamental to field-effect transistor fabrication.
Conventional MOS processes may use silicon dioxide as the gate dielectric, while many advanced devices use high-k dielectrics and metal gates. Planar transistors, FinFETs, and gate-all-around devices require different fabrication sequences rather than one universal FEOL recipe.
Choosing Silicon Wafers for FEOL Research
Selecting silicon wafers for semiconductor processing starts with the device design and the fabrication facility’s requirements. Important specifications include:
- Wafer diameter and thickness compatible with processing equipment.
- Crystal orientation appropriate for the device and etching process.
- Conductivity type and dopant, including p-type and n-type doped silicon.
- Silicon wafer resistivity matched to the intended electrical behavior.
- Surface finish, flatness, cleanliness, and contamination limits.
- Required oxide thickness or other starting surface layers.
Some device architectures use silicon-on-insulator (SOI) wafers, which contain a silicon device layer above a buried insulating layer. SOI and bulk silicon require different substrate specifications and process integration choices.
FEOL vs. MOL vs. BEOL
FEOL forms the semiconductor devices. Middle-of-line (MOL) processing generally creates contacts and local connections to those devices. Back-end-of-line (BEOL) processing builds the multilayer wiring that connects them into circuits. The exact boundaries between these stages can vary with the manufacturing process.
Understanding the FEOL Process Flow
A front-end-of-line process flow turns a prepared semiconductor substrate into an array of individual devices. Rather than completing each manufacturing operation only once, engineers repeat cleaning, patterning, deposition, etching, and thermal processing as different structures are built. The following examples explain important modules in silicon transistor fabrication; their order and details depend on the technology.
Device Isolation and Shallow Trench Isolation
Neighboring transistors need electrical isolation so that current follows the intended circuit paths. Shallow trench isolation (STI) creates insulating regions by etching trenches into silicon, filling them with dielectric material, and removing excess material through planarization. This separates active device areas while providing a surface suitable for subsequent processing.
Well Formation and Channel Engineering
In conventional bulk CMOS fabrication, wells provide regions with the electrical properties needed for n-channel and p-channel transistors. Selected dopants are introduced through patterned masks to control their location and concentration. The starting substrate doping and later implants serve different purposes: buying a doped silicon wafer does not replace the localized doping steps required by a device design.
Gate Dielectric and Gate Electrode Formation
The gate stack allows an applied voltage to control the transistor channel while limiting current through the gate dielectric. Thermally grown silicon dioxide is important in conventional MOS structures. Many advanced processes instead use hafnium-based high-k dielectrics with metal gate electrodes to maintain gate control while reducing leakage compared with an equivalently thin silicon dioxide dielectric.
Gate-first and replacement metal gate processes use different integration sequences. In a replacement gate flow, a temporary gate is formed and later replaced with the final gate materials.
Source, Drain, and Dopant Activation
Source and drain regions provide the carrier pathways on either side of the channel. Ion implantation can introduce dopants into selected areas, followed by annealing to activate them and repair crystal damage. Depending on the architecture, epitaxial growth may also help form engineered source and drain structures.
Why Lithography and Thin-Film Control Matter
Semiconductor photolithography determines where features are patterned, while etching transfers those patterns into selected layers. Alignment between successive patterns, feature dimensions, and etch profiles all influence whether the finished structures match the device design.
Equally important is control of thin-film deposition. Film thickness, composition, uniformity, and interface quality affect electrical behavior. Three-dimensional structures also require suitable coverage along sidewalls and around channels.
Planar MOSFETs, FinFETs, and Gate-All-Around Devices
FEOL processing changes with transistor geometry. A planar MOSFET has a channel near the wafer surface. A FinFET uses a raised semiconductor fin, allowing the gate to control the channel from multiple sides. A gate-all-around (GAA) transistor surrounds its channel with the gate; nanosheet devices are one example.
These architectures improve electrostatic control in different ways and require different combinations of patterning, selective etching, epitaxy, and gate formation. Research involving field-effect transistor substrates should therefore begin with the intended device structure and a compatible fabrication flow.
FEOL Process Challenges and Device Reliability
- Contamination: Particles and unwanted impurities can introduce defects or change device behavior.
- Surface and interface quality: Silicon wafer surface roughness and interface defects matter in surface-sensitive fabrication.
- Thermal budget: Temperature and processing time must support required reactions without excessive dopant redistribution or damage to existing layers.
- Dimensional control: Variations in channel geometry, gate dimensions, and film thickness can cause differences in electrical performance.
Matching Research Wafers to the Experiment
Prime grade silicon wafers are commonly selected when device fabrication requires tightly controlled substrate properties. Test grade silicon wafers may suit equipment qualification or individual process experiments, provided their specifications meet the experiment’s requirements. A wafer suitable for deposition testing is not automatically suitable for a complete transistor fabrication flow.
Frequently Asked Questions About FEOL
Does FEOL include chip packaging?
No. FEOL forms semiconductor devices on the wafer. Packaging occurs later, after wafer fabrication and subsequent processing and testing.
Is thermal oxide required for every transistor?
No. Dielectric materials depend on the device architecture. Conventional MOS structures may use thermal silicon dioxide, while advanced gate stacks often incorporate high-k materials.
Can SOI wafers be used for FEOL fabrication?
Yes. Silicon-on-insulator wafers support device fabrication in a silicon layer above a buried insulator. Device-layer thickness, buried oxide thickness, and electrical properties must match the intended process.
Related Semiconductor Fabrication Resources
- Silicon Wafers for Semiconductor Fabrication
- CMOS Silicon Wafers and Device Fabrication
- Field-Effect Transistor Substrates
- Photolithography Substrates and Applications
- Thermal Oxidation and Silicon Dioxide Layers
- Ion Implantation for Semiconductor Processing
- P-Type and N-Type Doped Silicon Wafers
- Thin-Film Deposition: PVD, CVD, and ALD
- Silicon Epitaxy and Epitaxial Growth
- Silicon-on-Insulator (SOI) Wafers